- Home
- Services
- Piping & Process Systems
- HDPE pipe welding
HDPE pipeline welding
HDPE pipe welding
Eleven butt fusion machines covering 20 mm to 1200 mm without a gap — and welders qualified under the German DVGW scheme to operate them.
A polyethylene joint is not an assembly — it is a weld, and once it is made the pipe either is or is not continuous. There is no gasket to replace and no flange to re-torque. Everything therefore rests on machine condition, operator competence and recorded parameters.
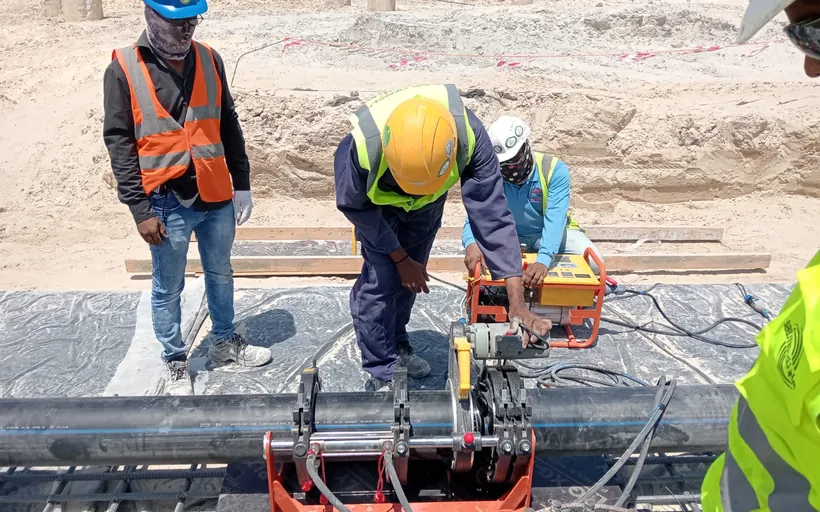
We hold eleven butt fusion machines giving continuous coverage from 20 mm to 1200 mm, with third-party calibration on the units that carry critical work. Welding is supervised under SKZ DVGW GW 331, the German certified-supervisor standard for HDPE pipe welding.
Diameter coverage without a gap
The reason the fleet is structured this way is that diameter gaps force sub-hire, and sub-hired machines arrive with unknown calibration and unfamiliar operators. Every size from a 20 mm service connection to a 1200 mm trunk main is covered by a machine we own and a crew we trained.
Jointing methods
Butt fusion
The primary method for straight runs and the one that produces the strongest joint. Pipe ends are faced, aligned, heated against a controlled plate, and fused under recorded pressure. Heating time, soak, changeover and cooling are all parameter-controlled and logged.
Electrofusion
Used for repairs, tie-ins, branch connections and locations where a butt fusion machine cannot be positioned. Four electrofusion units — Fox Eurotech and Ritmo Elektra — with calibration certificates current through March 2027.
Where this gets used
- Seawater intake and outfall pipelines
- Cooling water and chiller circuits, including conversion from metallic systems
- Potable and treated water distribution mains
- Firewater ring mains
- Storm water and drainage networks
- Chemical dosing and effluent lines
| Machine | Range | Calibration |
|---|---|---|
| KF-BF/200 | 20 – 63 mm | — |
| Ritmo BF/200 | 40 – 200 mm | — |
| WP200C manual | 63 – 200 mm | Third-party |
| KF-BF/250 | 63 – 250 mm | — |
| WP250B hydraulic | 75 – 250 mm | — |
| Worldpolly BF/315 | 90 – 315 mm | — |
| Rothenberger SHD 315 | 90 – 315 mm | Third-party |
| KF-BF/450 | 200 – 450 mm | — |
| Worldpolly BF/500 | 225 – 450 mm | — |
| Worldpolly BF/630 | 355 – 630 mm | Third-party |
| Bada SHBD710-1200 | 630 – 1200 mm | — |
Standards we work to
- DVS 2207-1
- DVS 2207-4
- ISO 21307
- ISO 12176-1
- ISO 12176-2
- SKZ DVGW GW 331
- ISO 4427
Common questions
What clients ask before awarding
What diameter range can you weld?
Are your welders certified?
Do you provide fusion records?
Can you work inside an operating plant?
Do you supply the pipe as well as weld it?
Send us the drawings. We will tell you what it takes.
BOQ, isometrics, specifications or a full tender package. Acknowledged within one working day, with the machine schedule and programme in the offer.